IQOQ Explained: IQ/OQ Guide for Automation & Control Systems

If you work anywhere near pharmaceutical manufacturing, biotech, food production, or any regulated industrial environment, you’ve run into the term IQOQ.

It shows up on equipment purchase orders, in validation master plans, and in emails from quality assurance asking, “Where’s the IQOQ documentation for this skid?”

For control systems engineers coming from a general industrial automation background, IQOQ can feel like a different language layered on top of familiar work.

Commissioning, testing, and documenting a system you already know how to build. That’s not far off.

IQOQ is essentially rigorous, auditable commissioning, done in a specific order, with paper trails that regulators can trust.

This guide breaks down what IQOQ means, how it applies to PLCs, HMIs, and building/process control systems, and where engineers commonly trip up.

What Does IQOQ Stand For?

IQOQ is shorthand for Installation Qualification (IQ) and Operational Qualification (OQ), two phases in the equipment and system validation lifecycle used in regulated industries such as pharmaceuticals, medical devices, food and beverage, and biotechnology.

  • Installation Qualification (IQ) confirms that equipment and systems are installed correctly, according to the manufacturer’s specifications and the approved design documentation.
  • Operational Qualification (OQ) confirms that the equipment operates as intended, across its specified operating ranges, once it’s installed.

Together, IQ and OQ form documented, objective evidence that a piece of equipment a PLC-controlled skid, an HVAC system, a filling line, or a cleanroom air handler was built right and works right before it’s ever used to make or handle a regulated product.

IQOQ almost always sits inside a broader validation framework that also includes:

  • DQ: Design Qualification: confirms the design meets user requirements before anything is built or installed
  • PQ: Performance Qualification: confirms the system performs consistently under real production conditions, with real product, over time

So the typical sequence an automation engineer will encounter is DQ → IQ → OQ → PQ, sometimes bundled and referred to loosely as “IQOQ” or “IQ/OQ/PQ” depending on the site’s quality system.

Why IQOQ Exists

Regulators, the FDA, EMA, and equivalent bodies, don’t take a manufacturer’s word that a system works.

They require documented proof. This comes from Good Manufacturing Practice (GMP) requirements and, in the US, guidance from 21 CFR Part 211 for pharmaceutical manufacturing and process validation expectations under the FDA’s process validation guidance.

For control systems specifically, IQOQ answers two blunt questions an auditor will ask:

  1. Is this system built the way it was supposed to be built?
  2. Does it perform as intended, reliably, across its full operating range?

If you can’t answer both with signed, dated, reviewed documentation, the system and potentially the product it touches aren’t considered validated, regardless of how well it actually runs on the floor.

Installation Qualification (IQ): What Gets Checked

IQ is a physical and documentation-level verification. It happens after installation but before the system is powered up and tested functionally. A typical IQ protocol for a control system or automated skid verifies the following.

  • Equipment identification: correct model, serial numbers, and revision levels match purchase specifications
  • Component verification: PLCs, HMIs, sensors, actuators, VFDs, and I/O modules match the approved bill of materials
  • Installation conditions: wiring, grounding, panel layout, and enclosure ratings meet the design drawings and applicable codes (NEC, NFPA 70, or local equivalents)
  • Utilities and services: power supply specifications, compressed air, network connections, and instrument air match design requirements
  • Software and firmware: Correct PLC program version, HMI application version, and firmware revisions are installed and match the released, version-controlled source
  • Calibration status: instruments (sensors, transmitters, gauges) have current, traceable calibration certificates
  • Drawing accuracy: as-built P&IDs, electrical schematics, and network architecture diagrams match what’s physically installed
  • Documentation package: manuals, spare parts lists, and vendor certificates are on file

IQ is asking, “Is this exactly what we specified, exactly where and how we specified it?” Nothing is tested for function yet. This step is purely about installed correctness.

Operational Qualification (OQ): What Gets Checked

Once IQ is signed off, OQ verifies the system actually functions correctly across its intended operating range.

For control systems, this phase is where an automation engineer’s normal commissioning instincts map directly onto the qualification protocol. OQ typically covers:

Functional testing of control logic

Every interlock, alarm, permissive, and sequence step is tested against the functional specification, including edge cases.

Alarm and interlock verification

High/low setpoints, safety interlocks, and critical alarms trigger correctly and at the correct thresholds.

Operating range testing

The system is exercised across its full specified range (temperature, pressure, speed, flow), not just at nominal setpoints.

Failure mode testing

What happens on power loss, sensor failure, communication loss, or E-stop, and whether the system fails to a safe state.

User access and security

Login levels, audit trails, and electronic records comply with requirements like 21 CFR Part 11 where applicable

Recipe and setpoint verification

For systems with recipe-driven control, confirming parameters load and execute correctly

Data integrity checks

Confirming logged data, alarms, and audit trails are accurate, timestamped, and tamper-evident.

If IQ confirms “it’s built right,” OQ confirms “it does what it’s supposed to do, every time, across the full range it’s designed for.”

A system can pass IQ and still fail OQ. For example, wiring and components match the drawings perfectly, but an interlock doesn’t trip at the specified setpoint because of a logic error or a miscalibrated sensor.

IQOQ vs. PQ: Where the Line Is

This distinction trips people up constantly, so it’s worth being precise.

Qualification StageCore QuestionWhen It HappensTypical Test Conditions
IQ (Installation)Is it installed correctly?Right after installation, before power-up testingStatic visual/documentation checks
OQ (Operational)Does it function correctly across its range?After IQ passes, before production useDynamic system run empty or with test media, across full operating range
PQ (Performance)Does it perform consistently in real production?After OQ passes, using real product/processDynamic real product, real production conditions, multiple runs

OQ tests the system’s capability to maintain setpoints, while PQ assesses whether the batch consistently meets specifications during operation.

OQ is largely engineering-driven; PQ usually pulls in process and quality teams more heavily.

A Simplified IQOQ Protocol Structure

Most IQOQ protocols, regardless of industry, follow a similar document skeleton:

  1. Purpose and scope: what system, what boundaries.
  2. Roles and responsibilities: who executes, who reviews, who approves.
  3. Prerequisites: training completed, documentation available, calibration current.
  4. IQ test cases: numbered, with acceptance criteria and space for actual results.
  5. OQ test cases: numbered, with acceptance criteria, expected results, and actual results.
  6. Deviation log: any failed test case, its root cause, and resolution.
  7. Summary and approval: sign-off from engineering, quality, and often the equipment owner.

Every test case needs a predefined, objective acceptance criterion written before testing starts. “Alarm triggers at 85°C ± 1°C and displays on HMI within 2 seconds” is a testable criterion. “Alarm works correctly” is not a testable criterion, and an auditor will flag it.

Common Places Engineers Get Tripped Up on IQ/OQ

Here are a few recurring issues from the field, especially for engineers new to validated environments.

Testing before documentation is finalized

If drawings or the functional specification changes after OQ testing starts, the protocol needs a formal deviation or revision. You can’t just quietly retest and move on.

Vague acceptance criteria

Every test step needs a specific, measurable pass/fail condition. “The system should respond appropriately” will get rejected in review.

Skipping failure mode testing

It’s tempting to only test the happy path. OQ specifically wants to see what happens when something goes wrong sensor failure, network dropout, power interruption and that the system fails safely.

Software version mismatches

The PLC program or HMI application tested during OQ must be the exact version that goes into production.

Any post-OQ code change, even a minor tweak, typically requires re-qualification of the affected functions.

Treating IQOQ as a one-time event

Significant changes to a validated system, a firmware update, a new sensor, or a logic change generally trigger a re-validation assessment, not just a change request in the maintenance log.

Who’s Involved in IQOQ Execution

IQOQ isn’t usually a solo effort. A typical execution team includes:

  • Automation/controls engineer: executes functional and logic testing, often writes the OQ test scripts.
  • Quality assurance: reviews and approves protocols and results and ensures compliance with the site’s validation master plan.
  • Equipment vendor/OEM: frequently supports or co-executes IQ, especially for skid-mounted or packaged systems.
  • Metrology/calibration team: provides calibration certificates and may execute instrument-specific checks.
  • Process/production engineering: defines operating ranges and acceptance criteria tied to actual process needs.

FAQ

Is IQOQ the same as commissioning?

No, though they overlap. Commissioning is the general process of getting a system running correctly.

IQOQ is the formal, documented subset of that work required for regulatory compliance in validated environments.

You can commission a system without ever generating IQOQ paperwork, but you can’t complete IQOQ without effectively commissioning the system first.

Does every control system need IQOQ?

No, IQOQ is required for equipment and systems that touch a regulated product or process in pharmaceutical, biotech, medical device, and certain food/beverage applications.

A general industrial or building automation system outside a regulated GxP environment typically doesn’t require formal IQOQ, though many companies apply similar rigor voluntarily for critical systems.

Who writes the IQOQ protocol, engineering or quality?

It’s usually collaborative. Engineering typically drafts the technical test cases based on design and functional specifications, while quality assurance reviews, standardizes format, and ensures the protocol meets the site’s validation procedures before execution.

What happens if a test case fails during OQ?

It gets logged as a deviation, investigated for root cause, corrected, and retested either the specific failed case or, depending on the site’s SOP, the full test sequence. The deviation and resolution become part of the permanent validation record.

Can IQ and OQ be combined into one document?

Yes, this practice is common, especially for smaller systems or less complex equipment. Hence the combined term “IQOQ.”

Larger or higher-risk systems often keep them as separate protocols executed sequentially.

The Bottom Line

IQOQ isn’t a separate skill set from good controls engineering. It’s controls engineering with the documentation discipline that regulated industries require.

If you already write clear functional specifications, test interlocks methodically, and version-control your PLC code, you’re most of the way to IQOQ-ready work.

The remaining gap is almost always documentation rigor: predefined acceptance criteria, traceable version control, and a paper trail an auditor who’s never met you can follow from design intent to tested result.

Best PLC Programming Books: Beginner to Advanced

Programmable logic controllers still run the physical world: conveyors, boilers, packaging lines, water treatment plants, and the building automation systems I work with every day.

And despite an ocean of YouTube tutorials and paid online courses, a good book remains the most cost-effective way to build the deep, structured understanding that makes you dangerous on the plant floor.

Books are typically priced between about $5 and $40 for eBooks (textbooks run higher). They’re written by people with decades of hands-on experience, and they don’t expire the moment a vendor pushes a software update.

The problem isn’t finding a PLC book. It’s finding the right one for where you are. A complete beginner needs plain-language fundamentals and ladder logic.

An engineer who already knows the basics needs vendor-specific depth or a structured text deep dive.

And every working automation professional eventually wants a reference book that lives on the desk for those “How does this instruction actually behave?” moments.

This guide sorts the best PLC programming books into three tiers: beginner, intermediate, and advanced/reference, so you can buy the one that matches your level instead of guessing. For each book, I note who it’s for, what’s strong, and what’s missing.

How to Choose a PLC Programming Book

Before the list, three quick filters that will save you money:

Match the book to the hardware you’ll actually touch

If you know you’ll be programming Allen-Bradley PLCs in Studio 5000 / RSLogix or Siemens in TIA Portal, a vendor-specific book beats a generic one every time. If you don’t know yet, start vendor-agnostic and specialize later.

Match the book to your learning style

Some books teach the why first (theory, control concepts, systematic understanding). Others are hands-on and get you writing ladder logic on page ten. Neither is better. They suit different people.

Buy used where possible

PLC fundamentals barely change year to year. A used copy of a canonical textbook at a fraction of the new price teaches the same ladder logic, timers, and counters as the current edition.

Beginner PLC Programming Books

These assume zero prior knowledge. Start here if terms like “rung,” “scan cycle,” and “normally open contact” are new to you.

Programmable Logic Controllers: Frank D. Petruzella

plc

This is the classic first-course textbook, used in engineering and technical programs for decades.

Petruzella focuses on how PLCs actually work and gives genuinely practical information on installing, programming, and maintaining PLC systems, deliberately complementing (not replacing) manufacturer manuals.

It teaches in a generic sense but leans on Allen-Bradley SLC 500 and ControlLogix instruction sets for its examples, so it doubles as a soft on-ramp to Allen-Bradley.

Topics are broken into small, digestible segments with review problems at the end of each chapter, covering everything from number systems and logic fundamentals through timers, counters, data manipulation, math instructions, installation, troubleshooting, and an intro to SCADA.

  • Best for: students, apprentices, and complete beginners who want a structured, classroom-grade foundation.
  • Strong: clear, systematic, well-illustrated; excellent breadth; a recognized standard.
  • Missing: It’s a textbook, so it’s pricier new. Buy an earlier edition used.

Beginner’s Guide to PLC Programming: Neal Babcock

A gentler, more conversational entry point than a full textbook, aimed squarely at people who just want to understand ladder logic and start writing simple programs without wading through control theory first. It’s widely circulated and has helped a lot of self-taught people get their first working program running.

  • Best for: self-study learners who want the fastest path to writing basic ladder logic.
  • Strong: approachable tone, practical focus, low friction.
  • Missing: limited depth on advanced topics. You’ll outgrow it, which is fine.

Bolton: Programmable Logic Controllers

W. Bolton’s compact introduction has been an entry-level standard, particularly in the UK and Europe, for years.

It covers basics through intermediate concepts in roughly 300 pages without the bulk of a full US textbook.

  • Best for: UK/European learners and anyone who prefers a concise book over a doorstop.
  • Strong: brevity and clarity; good value.
  • Missing: depth on advanced and vendor-specific topics.

Intermediate PLC Programming Books

You know the fundamentals: ladder logic, I/O, timers, counters. Now you want to go deep on a specific vendor platform or a specific language.

Allen-Bradley: RSLogix / Studio 5000 Practical Guides

If your shop runs Allen-Bradley, get a book built around your exact software environment. There are well-regarded practical guides specifically for RSLogix 5000 / Studio 5000 (ControlLogix and CompactLogix) and separate ones for the older RSLogix 500 (MicroLogix / SLC 500). Buy the one that matches your controller family.

The tag-based addressing in Logix 5000 is genuinely different from the file-based addressing in RSLogix 500, and a mismatched book will frustrate you.

  • Best for: engineers and technicians committed to the Allen-Bradley ecosystem.
  • Strong: hands-on walkthroughs of the actual IDE you’ll use daily; cheap eBooks.
  • Missing: Narrow by design, they won’t help you on a Siemens job.

Siemens: TIA Portal / S7-1200 & S7-1500 Guides

The Siemens equivalent. Look for books that walk through the TIA Portal environment and target the S7-1200 (for smaller applications) or S7-1500 (for larger/higher-performance ones).

Good ones cover hardware configuration, tag handling, and diagnosing common fault and error codes, the kind of practical friction that generic books skip.

  • Best for: engineers working in Siemens-heavy plants (common in Europe and multinational manufacturing).
  • Strong: platform-specific configuration and troubleshooting details.
  • Missing: again, single-vendor scope.

PLC Controls with Structured Text (ST)

Once you move beyond ladder logic, structured text is the language you’ll reach for on complex logic, math, and reusable function blocks.

A dedicated ST book is the cleanest way to learn it well, and it’s widely regarded as the go-to for that language specifically.

Because structured text is part of the IEC 61131-3 standard, what you learn transfers across vendors far better than ladder-only knowledge.

  • Best for: intermediate programmers ready to write cleaner, more maintainable code.
  • Strong: focused, transferable, increasingly relevant as projects grow more complex.
  • Missing: it’s language-specific; you still need the platform knowledge from the vendor books above.

Advanced & Reference PLC Programming Books

These are the desk books, the ones you don’t read cover to cover but reach for when you hit a specific, gnarly question.

Programmable Logic Controllers: An Emphasis on Design and Application: Kelvin Erickson

Version 1.0.0

A more rigorous, engineering-school treatment that goes past “how to write a rung” into system design, application patterns, and the reasoning behind good architecture. This is the book for engineers who want to design robust automation systems, not just make a light turn on.

  • Best for: degree-track engineers and anyone moving into system design responsibility.
  • Strong: design methodology and depth beyond typical intro texts.
  • Missing: heavier going; not a gentle first read.

Programmable Logic Controllers: Khaled & Eman Kamel

A thorough technical resource that bridges theory and hands-on practice across industrial automation systems, including more advanced programming techniques such as structured text. It’s substantial enough to serve as a long-term reference.

  • Best for: learners who want theory and practice in one comprehensive volume.
  • Strong: breadth, technical depth, staying power on the shelf.
  • Missing: less “quick start,” more “sit down and study.”

An IEC 61131-3 Reference

IEC 61131-3 is the international standard that defines the five PLC programming languages (ladder diagram, function block diagram, structured text, instruction list, and sequential function chart).

A dedicated reference on the standard is invaluable once you’re working across multiple vendors or writing portable, standards-compliant code. This is reference material, not a tutorial. You’ll consult it, not read it front to back.

  • Best for: senior engineers, integrators, and anyone working across mixed-vendor sites.
  • Strong: vendor-neutral authority; the definitive source on language behavior.
  • Missing: dry and technical, exactly what a reference should be.

Comparison Table: Best PLC Programming Books by Level

BookLevelBest ForVendor Focus
Petruzella: Programmable Logic ControllersBeginnerStudents, apprenticesGeneric (AB examples)
Babcock: Beginner’s Guide to PLC ProgrammingBeginnerFast self-studyGeneric
Bolton: Programmable Logic ControllersBeginnerConcise UK/EU introGeneric
RSLogix / Studio 5000 practical guidesIntermediateAllen-Bradley shopsAllen-Bradley
TIA Portal / S7 guidesIntermediateSiemens shopsSiemens
PLC Controls with Structured TextIntermediateLearning STVendor-neutral language
Erickson: Emphasis on Design and ApplicationAdvancedSystem designersGeneric
Kamel & Kamel: Programmable Logic ControllersAdvancedTheory + practice referenceGeneric
IEC 61131-3 referenceAdvancedCross-vendor / integratorsStandard

A Suggested Learning Path

If you’re starting from zero and want a concrete route:

Foundations

Read Petruzella (or Babcock if you want something lighter) to understand how PLCs work, ladder logic, and the scan cycle.

Specialize

Pick up the vendor guide for the hardware you’ll actually use: Allen-Bradley or Siemens. This is where you go from “understands PLCs” to “can program this PLC.”

Level up your code

Work through a structured textbook to write cleaner, more scalable logic.

Keep on the desk

Add a design-focused book (Erickson or Kamel) and an IEC 61131-3 reference as career-long companions.

    Pair whichever books you choose with actual practice. A free PLC simulator or a cheap trainer kit turns passive reading into muscle memory faster than anything else.

    Reading about a timer instruction and watching one misfire in simulation are two very different levels of understanding.

    Frequently Asked Questions

    What is the best PLC book for absolute beginners?

    For a structured, classroom-grade foundation, Petruzella’s Programmable Logic Controllers is the standard first-course text.

    If you’d rather have something lighter and faster, Neal Babcock’s Beginner’s Guide to PLC Programming gets you writing ladder logic sooner with less theory.

    Should I buy an Allen-Bradley or Siemens book?

    Buy for the hardware you’ll actually use. Allen-Bradley dominates North American manufacturing; Siemens is more common in Europe and many multinational plants.

    If you don’t know yet, start with a vendor-agnostic book and specialize once you know your platform.

    Do I need to learn structured text, or is ladder logic enough?

    Ladder logic is the best place to start and is enough for a lot of discrete control. But as projects get more complex, heavy on math, data handling, and reusable function blocks, structured text becomes far cleaner.

    Because it’s part of the IEC 61131-3 standard, structured text also transfers well between vendors.

    Are free PLC programming PDFs worth it?

    Some canonical texts circulate freely online, and they’re genuinely useful for fundamentals.

    Just make sure you’re getting a version that matches the software you’ll use, and buy a current edition if you need up-to-date vendor specifics or want to support the authors who write these books.

    Can I learn PLC programming from books alone?

    You can build strong theoretical knowledge from books alone, but pairing them with a simulator or a trainer kit is what makes it stick.

    Automation is a hands-on discipline. The books give you the map, and the practice gives you the terrain.

    Want to go deeper on the systems these controllers plug into? Explore our guides on BACnet, Modbus, and building management systems here on Control Circuitry.

    Digital vs Analog Signals in Industrial Automation

    Industrial automation systems depend on reliable signal transmission mechanisms. Sensors continuously measure physical variables within dynamic process environments. These measured quantities must be transmitted accurately to controllers. 

    Two fundamental signal categories dominate industrial communication architectures. These categories are analog signals and digital signals.

    Each signal type exhibits distinct characteristics and engineering implications. The selection between them influences system accuracy and reliability. 

    Noise immunity and scalability are also strongly affected. Modern facilities frequently integrate both signal types strategically.

    Engineers must evaluate operational requirements before final implementation decisions. 

    This article reviews the principles of digital and analog signals, their technical differences, and performance characteristics within industrial automation systems. It furthermore studies the advantages, limitations, and practical applications.

    Fundamentals of Industrial Signals

    Industrial operations produce constantly changing physical events that need exact measurement.

    Temperature, pressure, flow, and level vary depending on operating circumstances and process needs. 

    These physical characteristics are transformed into electrical representations ideal for transfer by sensors.

    From cables or networks, these electrical signals move toward control equipment for analysis. 

    Vibration, extremes in temperature, and electromagnetic interference notwithstanding, signal integrity has to be kept.

    Installations with big motors and switching equipment are usually subject to electromagnetic interference. 

    Correct grounding, shielding, and routing techniques greatly lower unwelcome signal distortions.

    The consistency of the signal and the general reliability of the measurement are also affected by transmission distance.

    Raw sensor signals are made ready for precise controller reading by signal conditioning modules. 

    Filtering, amplification, and isolation methods increase consistency and shield delicate components.

    Usually categorized as analog or digital, signals in industrial settings are. Every category has particular interpretation traits and transmission behavior influencing system design.

    Analog Signals in Industrial Automation

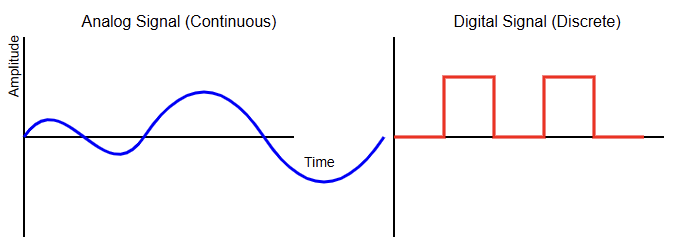
    Analog signals vary continuously over time and proportionally represent measured quantities.

    Their amplitude directly corresponds to the magnitude of the physical variable being monitored.

    In industrial practice, voltage or current levels change proportionally with process conditions. 

    One of the most widely adopted standards is the 4–20 milliampere current loop. This current loop configuration offers excellent immunity to electrical noise and voltage drops. Voltage-based analog signals typically range between zero and ten volts in control systems. 

    Analog transmission allows representation of virtually infinite intermediate values within a defined range.

    Sensor quality and internal conversion precision within the controller directly influence measurement resolution. 

    Still, attenuation and environmental effects can attack analog signals over great distances.

    Temperature variation and cable resistance may introduce small but significant measurement errors. 

    Signal isolators and repeaters help mitigate ground loop problems and improve reliability. Despite certain limitations, analog signals remain dominant within process industries requiring continuous measurement.

    Continuous control loops benefit greatly from proportional signal representation and smooth feedback behavior.

    Digital Signals in Industrial Automation

    Digital signals operate using discrete states, typically representing binary conditions of zero or one.

    A digital input may indicate whether a motor is running or stopped. Another digital signal might confirm that a valve has reached its fully open position. 

    Unlike analog signals, digital values change abruptly between defined logical levels. This discrete behavior makes them inherently less susceptible to gradual signal degradation. Minor electrical noise rarely alters logical states when thresholds are properly defined. 

    Digital communication in industrial automation extends beyond simple on-off signaling. Fieldbus and industrial Ethernet protocols transmit structured digital data packets efficiently.

    Examples include Modbus, Profibus, and Ethernet-based industrial communication systems. 

    These protocols encode multiple variables, diagnostics, and device parameters simultaneously.

    Error detection mechanisms, checksums, and sequence validation improve transmission reliability significantly. 

    Digital systems also support advanced diagnostics and device identification capabilities. Discrete signaling simplifies fault detection, troubleshooting, and system expansion within complex installations.

    Signal Conversion and Interface Considerations

    Industrial controllers must interpret both analog and digital signals reliably. Analog-to-digital converters transform continuous values into numerical representations for processing. Digital-to-analog converters generate proportional output signals for actuators and drives. 

    Programmable controllers typically contain integrated conversion modules for signal handling.

    Sampling rate strongly influences the accuracy of analog measurements in dynamic processes.

    Higher sampling frequencies capture rapid variations more effectively and reduce aliasing errors.

    Quantization introduces small approximation differences that depend on converter resolution.

    Resolution is determined by the number of bits used in conversion hardware. A twelve-bit converter provides moderate precision suitable for many applications. 

    Greater bit depth increases measurement granularity and control sensitivity. Signal scaling aligns raw digital counts with meaningful engineering units for operators.

    Calibration procedures ensure long-term measurement stability and regulatory compliance. Interface design, therefore, plays a critical role in overall automation system performance.

    Noise Immunity and Reliability

    Industrial environments contain significant electromagnetic disturbances generated by heavy equipment.

    Large motors, variable frequency drives, and switching devices produce electrical interference. Analog signals can pick up induced voltages along improperly shielded cables.

    Shielded twisted pair wiring significantly reduces electromagnetic coupling effects. Current loop systems inherently provide superior noise rejection compared to voltage signals. Digital signals resist minor amplitude distortions due to defined logical thresholds. 

    However, severe interference may corrupt digital data packets during transmission. Error detection algorithms quickly identify corrupted messages and request retransmission. Redundant communication paths further increase network availability and resilience. 

    Grounding strategy remains critically important for both analog and digital installations. Isolation barriers prevent hazardous potential differences and equipment damage.

    Reliability ultimately depends on disciplined engineering practices and proper installation procedures.

    Accuracy and Resolution Comparison

    Analog systems theoretically allow infinite resolution within a specified measurement range.

    In practice, achievable accuracy depends on sensor characteristics and conversion hardware limitations. 

    Component aging and environmental stress may gradually reduce measurement precision.

    Digital sensors often incorporate internal signal processing and compensation algorithms. These devices may provide stable outputs with reduced drift over time. 

    Resolution in digital systems becomes defined by word length and scaling configuration. Higher resolution enables finer control adjustments and improved process optimization.

    However, excessive precision may exceed realistic process requirements and increase cost unnecessarily.

    Engineers must carefully balance accuracy expectations with economic considerations. Calibration intervals significantly influence long-term confidence in measurement data.

    High reliability is attainable with either analog or digital architectures if properly designed. Selection should therefore reflect operational demands and performance objectives realistically.

    Transmission Distance and Infrastructure

    Long-distance transmission presents challenges for certain analog voltage signals. Signal drop increases proportionally with cable length and conductor resistance.

    Current loop systems maintain stable measurement integrity across longer distances effectively. 

    Digital communication networks support distributed architectures spanning extensive industrial sites.

    Industrial Ethernet enables reliable data exchange across large facilities and remote areas.

    Fiber optic links eliminate electromagnetic interference concerns in harsh environments. 

    Infrastructure cost strongly influences overall system architecture decisions. Existing plant wiring may favor retention of analog loops during modernization efforts. New installations frequently adopt digital networks for scalability and diagnostics. 

    Hybrid systems often integrate both approaches to optimize performance and cost. Scalable architecture supports sustainable long-term investment strategies.

    Integration with PLCs

    Programmable logic controllers interpret industrial signals using deterministic execution cycles.

    Manufacturers such as Siemens provide modular input and output interface cards for flexibility.

    Another major automation supplier is Rockwell Automation, offering comprehensive controller platforms. 

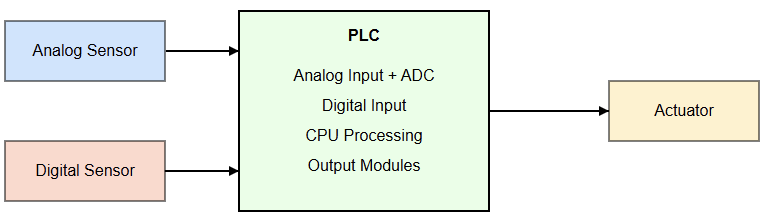
    Analog input modules precisely measure current or voltage from field instruments. Digital input modules detect discrete device states, such as switches and relays. Output modules drive actuators, solenoids, and motor contactors accordingly.

    Controller scan cycles process digital states extremely rapidly and predictably. Analog values require sampling, scaling, and filtering before logical evaluation. Distributed input systems reduce centralized wiring complexity and installation cost. 

    Networked architectures enhance diagnostic visibility and configuration flexibility significantly.

    Modern controllers often combine standard control and safety functions within integrated platforms.

    Effective signal management remains fundamental to automation system reliability and performance.


    PLC Signal Integration Architecture

    Applications Across Industrial Sectors

    Analog Applications

    Process industries such as chemical manufacturing rely heavily on analog instrumentation.

    Flow transmitters provide continuous feedback to closed-loop control systems. Pressure monitoring ensures safe equipment operation under varying load conditions. 

    Digital Applications

    Digital signals supervise pump status, interlocks, and alarm conditions reliably. Power generation facilities integrate extensive measurement networks for turbine control. Oil and gas installations deploy advanced distributed control architectures. 

    Mixing Applications

    Food processing lines combine continuous measurement with discrete packaging machinery control.

    Water treatment facilities monitor the level continuously. They also constantly supervise turbidity and chemical dosing.

    Each industry carefully balances analog and digital implementation according to operational needs. 

    Maintenance teams analyze both continuous trends and discrete event logs. Operational safety and productivity depend on accurate signal interpretation.

    These diverse applications demonstrate the complementary nature of both signal types.

    System Design Strategy and Hybrid Approaches

    Modern automation strategies rarely rely exclusively on one signal category. Hybrid architectures combine analog measurement reliability with digital communication flexibility. Critical feedback loops often maintain analog proportional control for stability. 

    Supervisory systems exchange information and diagnostics through digital networks. Gradual modernization strategies minimize disruption within operating facilities. Legacy analog instruments frequently coexist with intelligent digital field devices.

    Planning for migration guarantees compatibility with upcoming technical breakthroughs. Engineers assess performance goals, lifecycle cost, and maintainability demands. 

    Traceability and regulatory compliance are aided by configuration management and documentation.

    Balanced system design improves operational resilience and long-term scalability. Effective integration ultimately determines overall automation success.

    Conclusion

    This article introduced the principles of digital and analog signals in industrial automation.

    It explained their characteristics, operational behavior, integration considerations, and practical applications across diverse industrial sectors. 

    Analog signals provide continuous proportional representation of changing process variables.

    Digital signals deliver discrete states and structured communication with advanced diagnostics.

    Each approach offers distinct strengths regarding noise immunity, scalability, and system integration. 

    Environmental conditions and transmission distance significantly influence performance outcomes.

    Programmable controllers integrate both signal types within cohesive architectures. Hybrid implementations often achieve an optimal balance between reliability and flexibility.

    Engineers must align the signal strategy with the documented process requirements carefully.

    Thoughtful planning ensures dependable, efficient, and future-ready automation infrastructure.

    Understanding these distinctions enables informed technical decisions and improved industrial system performance.

    FAQs: Digital vs Analog Signals in Industrial Automation

    In industrial automation, what is an analog signal? 

    Process values are represented by an analog signal that changes constantly and proportionally. 

    Automation systems define a digital signal as 

    Information is sent through discrete binary states in a digital signal. 

    What kind of signal gives greater noise immunity? 

    Usually, digital signals are more resilient to little electrical disturbance are digital signals. 

    Why are 4–20 mA loops so widely used? 

    Their robust noise immunity enables dependable long-distance communication. 

    Can both signal kinds function within one control system? 

    Most modern automation systems do so efficiently.

    What is a Fail-Safe System in Automation?

    Industrial automation systems require increasing levels of operational dependability and safety.

    Modern systems feature sophisticated equipment with mechanical, electrical, and thermal hazards.

    Engineers have to simultaneously safeguard production continuity, equipment, and personnel. 

    Engineers must protect personnel, equipment, and production continuity simultaneously. Conventional control strategies alone cannot guarantee acceptable risk reduction. For this reason, protective mechanisms are integrated into automation architectures. 

    Among these mechanisms, fail-safe systems hold critical importance. They ensure predictable behavior when faults or abnormal conditions occur.
    Instead of maximizing productivity during failure, they prioritize safety outcomes. 

    Their design philosophy assumes that components can and will fail. Understanding fail-safe principles is essential for responsible automation engineering practice.
    This article reviews the concept of fail-safe systems, their design philosophy, architectural principles, standards compliance, and practical industrial applications.

    Fundamentals of Automation Control Systems

    Industrial automation relies on deterministic control executed by programmable devices. Controllers receive input signals from sensors distributed across machinery. These inputs represent temperature, pressure, position, or safety status.

    The controller processes signals using predefined logical algorithms. Outputs then command actuators such as motors, valves, and contactors. Standard control systems emphasize efficiency, availability, and productivity optimization.

    They are widely deployed in manufacturing. Also, they are utilized in water treatment sectors and energy facilities.

    Vendors such as Siemens and Rockwell Automation provide global automation platforms. These systems typically focus on maintaining continuous process operation.

    However, continuous operation is not always the safest outcome. When abnormal conditions arise, protective intervention becomes necessary.
    Fail-safe systems address this requirement by ensuring controlled shutdown. They complement standard control layers within hierarchical automation architectures.

    What is a Fail-Safe System in Automation?

    A fail-safe system is engineered to default to a safe state. This transition occurs automatically when a fault is detected.

    The safe state minimizes risk to humans and equipment. Unlike conventional systems, performance during failure is not prioritized.

    Instead, predictable hazard mitigation becomes the primary objective. A fail-safe design anticipates power loss and component malfunction. Outputs are typically de-energized to eliminate hazardous motion. 

    For example, a motor contactor may drop out during failure. This prevents unintended mechanical movement or energy release. The principle applies across electrical, mechanical, and software domains. 

    Fail-safe systems are foundational elements of functional safety engineering. They contain and manage faults to prevent large-scale failure events.

    Relationship with Functional Safety Standards

    Fail-safe design principles align closely with international safety standards. The most recognized standard is IEC 61508 for electrical safety systems. Another widely applied machinery standard is ISO 13849.

    These standards define systematic processes for achieving risk reduction. They introduce measurable integrity metrics for safety functions. Designers must demonstrate that the dangerous failure probability remains acceptable.

    Compliance requires structured lifecycle documentation and verification. Hardware architecture must tolerate predictable fault conditions. Software development must follow validated and traceable methodologies.

    Fail-safe systems are therefore not arbitrary protective additions. They are carefully engineered to meet defined performance levels. Certification provides confidence in their reliability under hazardous scenarios.

    Core Design Philosophy of Fail-Safe Systems

    The fundamental philosophy assumes that failures are inevitable. Therefore, systems must respond safely rather than unpredictably. This mindset differs significantly from traditional reliability engineering.

    Reliability seeks uninterrupted performance under normal conditions. Fail-safe engineering focuses on controlled behavior during abnormal conditions. Designers intentionally define what “safe” means for each application.

    In many electrical systems, the safe state is de-energization. Springs may return mechanical components to neutral positions. Valves may close automatically when control pressure disappears.

    Electrical circuits often employ normally closed safety contacts. If wiring breaks, the circuit opens and stops operation.

    This arrangement ensures the detection of disconnection faults. Such design practices reduce the likelihood of hidden, dangerous failures. Predictable shutdown becomes a deliberate and verified outcome.

    Architectural Principles and Redundancy

    Redundancy is frequently integrated within fail-safe architectures. Dual-channel circuits monitor safety devices independently. Both channels must agree before hazardous motion is permitted.

    If disagreement occurs, the system initiates a shutdown. This structure reduces vulnerability to single-component failure. Some systems implement diverse processor architectures for added robustness.

    Safety controllers often compare execution results cyclically. Memory integrity checks are performed during each scan cycle.

    Input circuits detect short circuits and cross faults. Output circuits may monitor feedback from external relays. 

    These mechanisms collectively increase diagnostic coverage significantly.
    Architectural discipline distinguishes fail-safe systems from conventional controls. The objective remains minimizing undetected dangerous faults.